How a Montana CNC Shop Beat a 44-Hour Deadline with Tungaloy
I usually don't answer my phone after 3:30 on a Thursday. That's when the fake emergencies show up—the ones where somebody's deadline collapsed two weeks ago and somehow became my problem. But in March 2024, the call was real.
The Call That Started It
A purchasing manager from a medical device company was on the line. Her company builds aesthetic laser platforms, and their engineering team had spent weeks comparing CO2 vs IPL laser modules for a new handpiece. Honestly, that debate is above my pay grade. The 64 aluminum parts sitting on her inspection bench weren't.
Here's the part that stung. We'd quoted those same parts back in January, and our number came in about 30% higher than the vendor she chose. That vendor promised the same tolerance, same material, same turnaround—for less money. They delivered on the money. The threads didn't match the print, and the bore was out of round. These parts didn't need rework. They needed to be remade.
A 44-Hour Clock
“The parts have to be at our integrator Monday morning,” she said. “The only way to make that happen is Saturday's freight truck.” That gave us 44 hours, including the rest of Thursday.
I told her we'd look at the print and call back in twenty minutes. My first instinct, if I'm being honest, was no. The main bore had a tolerance of plus zero, minus five tenths—half a thousandth—and the internal thread had to pass a Go plug gage on every part. That's demanding on a normal week. With 44 hours, one lathe, and a part that had already failed at another shop, saying yes felt almost reckless.
She didn't try to negotiate. That's how I knew this was serious. She said, “If you can make them fit the print, send me the invoice.” So we said yes.
We're a CNC machining shop in Montana, not a huge one—eleven people, three machining centers, four lathes, and a stubborn belief that reliable tooling is cheaper than downtime. A growing part of our business is additive manufacturing accessories: nozzle adapters, thermal-break fittings, and other small precision parts for industrial 3D printers. That work has taught us to expect surprises on tight tolerances.
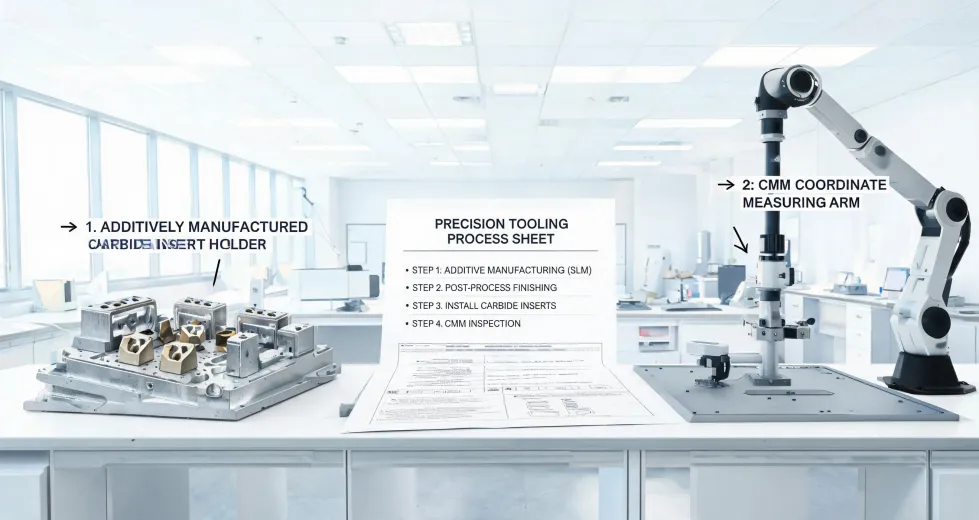
The material was 6061-T6 aluminum, and we had enough bar stock in the rack. The work looked like standard turning: face, drill, bore, thread, part off. Our lathes are set up with Tungaloy turning tools and Tungaloy tool holders precisely because a job like this doesn't leave time for second-guessing. When a tool holder sits on center and an insert indexes the same way every time, one variable disappears.
Tooling Isn't the Place for Surprises
By 8:30 that night, the first article was done. The bore gage said we were dead on. The Go plug gage dropped through the thread like it was supposed to. For a minute, I let myself believe the hard part was over.
It wasn't.
During the second-operation setup, we found the real problem. The outside diameter of the part was a sealing surface, so we couldn't grab it in a standard steel collet without marking it. Our normal solution would have been a custom aluminum fixture, but making one would eat four hours we didn't have.
So we did something that would have sounded ridiculous ten years ago. Our lead machinist modeled a split sleeve on his laptop, and about forty minutes later, we pulled it off the 3D printer we keep in the back of the shop. The sleeve held the part by the outside diameter, spread the clamping pressure evenly, and left no marks. That printed fixture saved the entire run.
We ran first operations until 2 a.m. Our night guy took over from there, and by six Saturday morning, every first operation was done. We finished the back operations, deburred each part by hand, and checked every thread with the gages. At 11:57, the freight driver loaded 64 parts into his truck.
The Real Price of a Cheap Quote
Monday morning, the customer called to confirm the parts arrived on time. She also said something I've repeated in meetings ever since:
“We already paid for the cheap parts,” she said. “They just didn't exist.”
People think a rush job is about speed. It isn't. It's about removing surprises. The tooling either behaves predictably or it doesn't. The fixturing either works the first time or it doesn't. The estimate either includes the real cost of failure or it doesn't.
That's why I use Tungaloy. I'm not going to claim it's the only brand that can hold a five-tenths bore—that would be false. But when every minute matters, I want the tooling I've tested. Tungaloy has been consistent for us, part after part, and consistency matters more than the small difference in insert price.
I think about that when I hear customers comparing CO2 vs IPL laser sources for their next product, too. It's human to compare list prices. But the real cost includes rework, missed deadlines, failed launches, and broken trust. The cheapest quote is only cheap if the parts actually fit.
Ana Kovacevic
Ana Kovacevic is an independent CNC milling and five-axis machining analyst covering precision parts, machining centers, workholding, and complex surface strategies. She applies ISO 1101 geometrical tolerancing while examining datum schemes, tool reach, setup count, spindle load, surface roughness, and inspection access before accepting tight requirements. Her technical guides help design and manufacturing teams improve DFM decisions, compare machine capability, and control dimensional risk from prototype through production.