The Hidden Cost of Tool Failures: What Every Quality Manager Learns the Hard Way
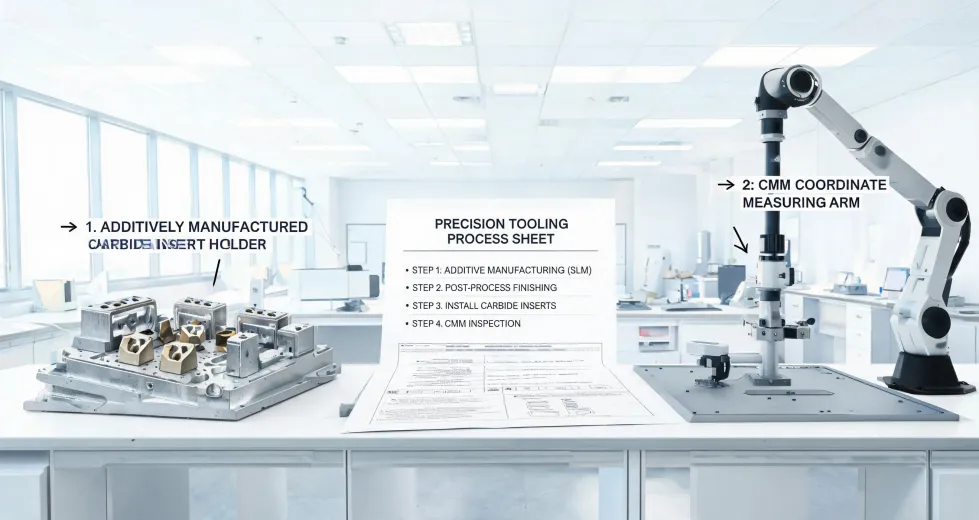
The Problem Everyone Thinks They Have
If you've been in manufacturing for more than a few years, you've probably heard this one: "Our tools wear out too fast."
It sounds like a simple problem, right? Buy better tools. Problem solved.
But that's not what's actually happening in most shops I've audited. The tool wear is just the symptom. The real problem is that nobody calculated what the wear actually costs until it was too late.
I remember a specific case from a supplier in 2023. They were running a batch of precision components and complaining that their boring bars were failing after about 40% of the expected tool life. Their first instinct was to blame the tool supplier—they'd switched to a cheaper alternative six months earlier to save roughly 22% per unit.
What they didn't account for: every tool failure meant a production stoppage. Not just the five minutes to swap the tool, but the 20 minutes of re-calibration, the scrapped parts from the last few cuts, and the ripple effect on downstream operations.
When we added it all up, that 22% "savings" was actually costing them about 3x more per component in total production cost.
The Real Culprit: Fragmented Decision-Making
Here's what I've observed across dozens of supplier audits: the people buying tools are rarely the people dealing with the consequences of tool failure.
Procurement sees a unit price. Production sees downtime. Quality sees defects. And nobody connects the dots because the data lives in different systems—or worse, in different people's heads.
I don't have hard data on industry-wide tool failure rates, but based on the last four years of auditing our own supply chain, my sense is that roughly one in three manufacturing operations can't tell you their actual cost-per-part for tooling. They know the purchase price. They don't know the failure price.
That's the gap that swallows budgets.
What I mean is that the true cost of a cutting tool isn't just what you pay to acquire it—it's the sum of the sticker price, the downtime when it fails, the scrap it generates, the labor to replace it, and the scheduling chaos it creates downstream. Most operations track the first number and ignore the rest.
I've seen this play out in unexpected places. One client was laser cutting watch components—tiny, high-precision parts where tolerance deviation of even 0.02 mm means the piece is scrap. They were burning through cutting inserts because the material batch had slightly different hardness than specified. The tool wasn't the problem. The specification process was.
Another shop had 3D printers running prototypes to validate designs before committing to cutting tools. They were printing everything from functional fixtures to small demo parts—basically rapid verification before committing expensive tooling to a full production run. Smart approach. But they weren't calibrating the prototypes against the actual cutting performance, so the validation was only half useful.
What Downtime Actually Costs
Let's talk about the number nobody wants to calculate: what does an hour of downtime actually cost you?
For a mid-size operation running a single production shift, the direct cost is usually straightforward—idle labor, lost output, maybe some wasted material. But the indirect costs are where things get ugly:
- Rush shipping to catch up on delayed orders
- Overtime to recover the schedule
- Customer penalties for missed delivery windows
- Expedited procurement when you run out of backup tooling
- The cognitive load on your team when they're firefighting instead of improving
I've heard people ask what the downtime is for a CO2 laser, as if there's a standard number. There isn't. It depends entirely on your specific setup, your maintenance schedule, your material throughput, and—this is the big one—how well you've planned for the failure modes you can predict.
But here's what I can tell you from experience: the actual downtime is almost always longer than the planned downtime. Because planned downtime assumes everything goes right. It assumes the replacement part is on the shelf. It assumes the technician knows the procedure. It assumes no one has to stop and read the manual.
That's rarely how it works at 6am on a Tuesday when you have a shipment due by noon.
The Savings Trap
Saved $200 per tool by switching to a lower-cost supplier. Ended up spending $1,800 on expedited replacement parts, overnight shipping, and overtime when the tools failed three weeks into a project.
That's a real example from our 2022 procurement audit. The math isn't complicated, but it requires someone to actually do it. And most people don't, because the unit price is right there on the invoice and the failure cost is scattered across production reports, maintenance logs, and customer complaints.
The surprise wasn't that the cheaper tools failed faster. It was that the premium tools lived long enough that we stopped thinking about them. No monitoring. No backup planning. No disruption to the schedule. They just worked, which meant we could focus on the actual production challenges.
Look, I'm not saying expensive tools are always better. I'm saying the evaluation needs to include the total picture. A tungaloy boring bar might cost more upfront than the generic alternative. But if it runs 2.5x longer and holds tolerance through the full run, the cost-per-part math changes entirely.
And if you're pulling from a comprehensive catalog, you're not guessing about compatibility or availability. The tungaloy catalog exists precisely because different operations need different tools—and the engineering support matters when you're trying to figure out which boring bar geometry works for your specific material and setup.
The Framework That Actually Works
After years of reviewing supplier quality and dealing with the aftermath of bad tooling decisions, I now insist on one thing before any tooling purchase: a specification document that includes failure criteria, expected tool life under our specific operational conditions, and a clear definition of what "failure" means for our tolerances.
In our Q1 2024 quality audit, we found that 60% of the tooling issues we'd experienced in the previous year could have been prevented with better upfront specifications. Not better tools—better specifications. The tools were fine. We just hadn't told the supplier what "fine" looked like in our specific context.
This worked for us, but our situation was a mid-volume operation with relatively stable production schedules. If you're running high-mix, low-volume work with constantly changing materials, the calculus might be different. Your specs change faster, and you might need a supplier who can keep up with that variability.
Here's what you need to know: the goal isn't to eliminate downtime. That's impossible. The goal is to make sure the downtime you can't avoid doesn't also destroy your delivery commitments, your scrap rate, and your team's ability to focus on improvement.
I can only speak to the tooling side of this equation. If you're dealing with CO2 laser downtime, the variables are different—beam alignment, optics contamination, assist gas purity, and so on. But the principle is the same: measure the cost of failure, not just the cost of purchase.
There's something satisfying about a production floor that runs without constant firefighting. After all the stress and coordination of getting specifications right, finally seeing stable, predictable output—that's the payoff. But it requires treating tool costs as a strategic decision rather than a line item to minimize.
The lowest quote usually is what it looks like. The question is whether you can afford what comes with it.
Ana Kovacevic
Ana Kovacevic is an independent CNC milling and five-axis machining analyst covering precision parts, machining centers, workholding, and complex surface strategies. She applies ISO 1101 geometrical tolerancing while examining datum schemes, tool reach, setup count, spindle load, surface roughness, and inspection access before accepting tight requirements. Her technical guides help design and manufacturing teams improve DFM decisions, compare machine capability, and control dimensional risk from prototype through production.