Tungaloy Cutting Tools & Tool Holders FAQ: HSS Roughing End Mills, Plastic Pallet Molds, and 3D Printing Services
-
What should I check first when specifying Tungaloy cutting tools?
-
Are Tungaloy tool holders worth the premium over generic holders?
-
When does an HSS roughing end mill make more sense than carbide?
-
What quality issues matter most in injection molding for plastic pallets?
-
How do cutting tools affect plastic pallet mold lead time?
-
What are the best 3D printing services for prototypes or fixtures?
-
Is rush delivery worth the extra cost when a mold deadline is tight?
-
What do buyers often overlook about tool holder runout?
I’m a quality and brand compliance manager at a custom machining company. I review every tooling package before it reaches customers—roughly 200+ items a year. I’ve rejected about 10% of first deliveries in 2024 due to spec mismatches or runout issues. This FAQ covers what I check on Tungaloy cutting tools, Tungaloy tool holders, HSS roughing end mills, injection molding for plastic pallets, and how I evaluate 3D printing services when they touch toolroom work.
- What should I check first when specifying Tungaloy cutting tools?
- Are Tungaloy tool holders worth the premium over generic holders?
- When does an HSS roughing end mill make more sense than carbide?
- What quality issues matter most in injection molding for plastic pallets?
- How do cutting tools affect plastic pallet mold lead time?
- What are the best 3D printing services for prototypes or fixtures?
- Is rush delivery worth the extra cost when a mold deadline is tight?
- What do buyers often overlook about tool holder runout?
What should I check first when specifying Tungaloy cutting tools?
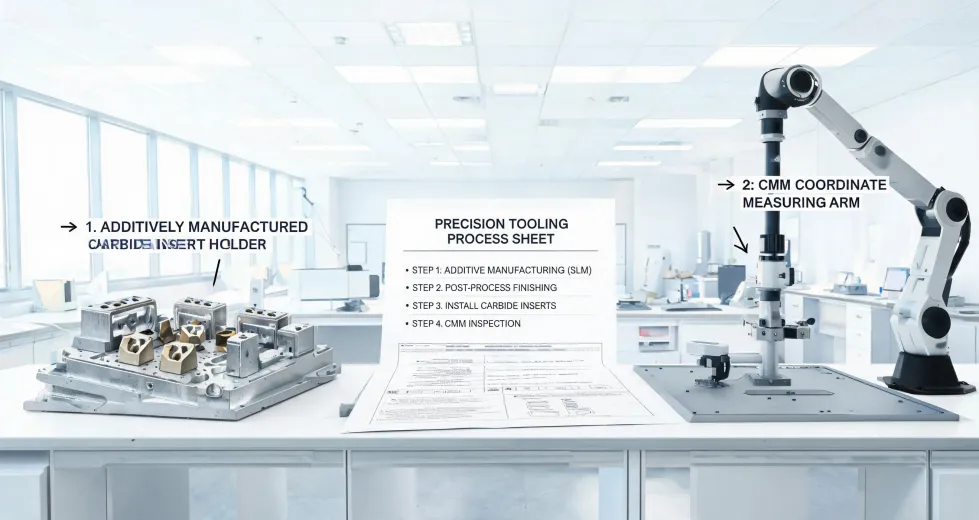
Start with the application, not the catalog page. I need workpiece material, hardness, machine taper, coolant type, and the feature tolerance that actually matters. For Tungaloy cutting tools, I verify the insert grade, chipbreaker, and corner radius against the operation—roughing vs finishing. According to Tungaloy’s public catalog (tungaloy.com), holders are organized by taper, projection, and runout class; check the exact class before ordering. I only started requiring a runout report after skipping it once and eating an $800 scrap charge. That mistake is why every Tungaloy tool holder order now includes a first-article check. Prices vary, so verify current rates.
Are Tungaloy tool holders worth the premium over generic holders?
Sometimes. It depends on spindle interface, runout tolerance, and how often you change tools. For our 5-axis cells, a Tungaloy tool holder with low runout reduced chatter on a deep boring job. Not a miracle, just more consistent. On a manual lathe doing one-off plastic pallet mold repairs, a generic holder was fine. So the question isn’t Tungaloy vs generic. It’s whether your process can tolerate runout variation. If you’re holding ±0.0005 in, pay for the certainty. If you’re at ±0.005 in, save the money. Harsh? Maybe. But that’s how I justify tooling spend.
When does an HSS roughing end mill make more sense than carbide?
HSS roughing end mills still make sense on older machines, low-RPM setups, and softer materials where toughness matters more than speed. In our shop, we keep HSS roughing end mills for aluminum fixtures and occasional plastic pallet mold repair plates—not for hardened mold steel. Carbide wins on rigidity and surface speed. HSS wins on cost and shock resistance. If I’m roughing a cavity for injection molding for plastic pallets and the setup is stable, I go carbide. If the operator is working around interrupted cuts and a less rigid setup, HSS can be the safer call. Not ideal for every job. Workable for the right one.
What quality issues matter most in injection molding for plastic pallets?
I’m not a polymer chemist, so I can’t tell you the best PP or HDPE grade. What I can tell you from a quality role is that dimensional consistency, mold finish, and gate location drive most complaints. For plastic pallets, warpage and wall-thickness variation show up fast under load. Tool wear on the mold cavity changes flow balance. That’s why I track cutter condition on the mold-making side. If the finishing tool leaves witness marks or the tool holder has runout, the molder inherits a problem. The best injection molding for plastic pallets starts with a mold that was cut to spec—not just quoted cheap.
How do cutting tools affect plastic pallet mold lead time?
More than most buyers expect. Roughing passes remove the bulk, but finishing passes determine whether the mold needs hand-polishing or EDM work. A worn Tungaloy cutting tool or a high-runout Tungaloy tool holder can add hours of spotting and rework. In Q3 2024, we switched one roughing operation from a generic cutter to a Tungaloy milling cutter and cut one shift off the schedule. If I remember correctly, the finish pass still needed adjustment—but the roughing was cleaner. The lesson: tooling choices are schedule choices. If your mold deadline is tight, don’t treat cutters as a commodity line item.
What are the best 3D printing services for prototypes or fixtures?
There’s no single best 3D printing service. It depends on material, tolerance, certification, and lead time. For toolroom fixtures, I care about dimensional stability and whether the vendor provides a first-article report. I don’t have hard data on industry-wide defect rates for 3D printed fixtures, but based on our last 18 months, roughly 1 in 6 parts needed rework when we skipped material certs. For prototypes, speed matters. For fixtures, repeatability matters. Ask for material data sheets, machine calibration records, and a clear lead-time guarantee. If the answer is ‘probably on time,’ that’s not a guarantee. Prices as of January 2025; verify current rates.
Is rush delivery worth the extra cost when a mold deadline is tight?
Yes—when the deadline is real. In March 2024, we paid $400 extra for rush delivery on a tool holder. The alternative was missing a $15,000 mold trial. That’s the trade. Rush fees buy certainty, not just speed. But I don’t pay rush premiums for ‘nice to have’ dates. I pay when a missed deadline stops a customer line or delays a pallet-mold validation. After getting burned twice by ‘probably on time’ promises, we now budget for guaranteed delivery on critical-path tooling. The cheap option that arrives late is the most expensive option. Not always, but often enough.
What do buyers often overlook about tool holder runout?
They treat it as a machine problem, not a tooling problem. Runout stacks: spindle, holder, collet, cutter. A Tungaloy tool holder with a good runout spec can still perform badly if the collet is worn or the spindle taper is dirty. I only believed this after ignoring it and scrapping a batch of bores—$1,200 gone (unfortunately). Now every setup sheet includes a runout check before first cut. Why does this matter? Because the tool holder is the easiest variable to control. If you skip it, you’re guessing. And in mold work, guessing gets expensive.
Prices and specifications are for general reference only. Verify current Tungaloy catalog data, tool holder tolerances, and vendor lead times before ordering.
Ana Kovacevic
Ana Kovacevic is an independent CNC milling and five-axis machining analyst covering precision parts, machining centers, workholding, and complex surface strategies. She applies ISO 1101 geometrical tolerancing while examining datum schemes, tool reach, setup count, spindle load, surface roughness, and inspection access before accepting tight requirements. Her technical guides help design and manufacturing teams improve DFM decisions, compare machine capability, and control dimensional risk from prototype through production.